How to Achieve CNC Tooling Cost Reduction: Splitting a Combined Drill Bit to Save $74,953 a Year
ROI cao bất thường vì vốn đầu tư đã khai rất nhỏ so với mức tiết kiệm hằng tháng.
Vấn đề thực trạng:
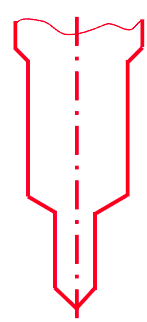
The part is an aluminum component whose function is to distribute cold air; it has a stepped hole (one large end, one small end) with a chamfer at the top where a tube is inserted and welded on. Each part has 5 holes of the same size, machined in one pass; the fixture holds 4 parts per cycle. This stepped hole is currently machined with a single integrated drill that cuts both Ø5 and Ø10 in one pass. The tool is carbide (required because the aluminum surface finish must be clean, with no burrs inside the hole). Machining is done on a KIRA CNC milling machine Problem: this integrated drill's tool life is highly unstable — ranging from as few as ~20 parts to as many as ~1,000 parts before it needs replacing, with no way to predict it.
Nguyên nhân gốc:
Two compounding technical causes: 1. Chips generated while drilling Ø5 and Ø10 are produced at the same time, so chip evacuation up from the main cutting edge is obstructed and chips build up inside the hole. 2. At the junction between Ø5 and Ø10, standard drill-grinding technique requires a chip-relief groove at exactly that point — which is also the point of highest structural stress, making the tool body weak exactly where it needs to be strongest.
Cơ chế cải tiến:
Reduce the amount of chip that must be evacuated in a single drilling pass. The only approach that truly solves this is to split the combined drill into separate, single-purpose tools
Giải pháp:
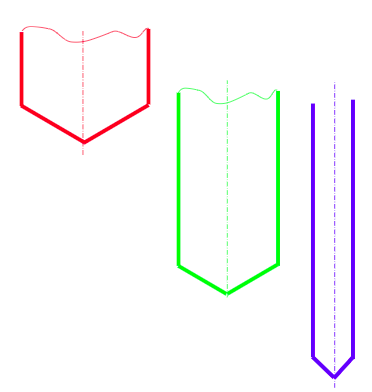
Split the 1 combined drill into 3 tools: 1. Centering drill — also does the chamfer. 2. Ø10 drill (large hole). 3. Ø5 drill (small hole). Machining sequence: Center → Drill Ø10 → Drill Ø5. Because Ø10 is drilled first, the actual drilling depth for the Ø5 tool becomes much shorter than before — this is the key factor that makes the Ø5 drill last longer.
Kết quả:
Trước cải tiến, các hạng mục chi phí đã khai trong đề án này tốn $6,446 mỗi tháng.
Sau cải tiến, cùng những hạng mục đó còn $200 mỗi tháng.
Mức tiết kiệm là $6,246 mỗi tháng, tương đương $74,953 mỗi năm — giảm 96.9% so với chi phí của chính những hạng mục đã khai trong đề án này (Dụng cụ (CONSUMABLE)), không phải so với toàn bộ giá thành sản phẩm.
Vốn đầu tư là $298, khai chi tiết thành 2 khoản trong bảng chi phí triển khai một lần.
Thời gian hoàn vốn là ~2 ngày.
Bài học kinh nghiệm:
Before arriving at the 3-drill split, several other approaches were tried first, because of the wish to avoid this level of investment: - Reducing feed rate (F): tool life barely improved, while cycle time got longer — not a worthwhile trade-off. - Under-tightened tool clamping at tool change: drills still broke despite careful tightening — but on review, the clamp holder's design clamping force is always well above what's needed, so this wasn't the real cause. - Leftover chip wrapped around the drill from the previous cycle: if an operator forgot to clear chips, the next cycle's centering pass would deflect off-axis because chips sat between the tool and the part surface. Addressed by enforcing 100% chip removal, building a machine fixture to auto-clear chips via the machining program, or using air blast. - Coolant/oil not spraying accurately or sufficiently at the cutting point: tried adjusting nozzle sizes multiple ways with no meaningful improvement.
Tri thức tái sử dụng
Điều kiện áp dụng:
- The mill needs enough tool magazine capacity for 3 tools instead of 1 (confirmed: KIRA KPC-30B has 20 ATC positions as standard, more than enough). - Upfront investment is fairly significant (extra BT30-ER32 tool holder + separate ER32 collets sized to each tool's shank, plus the tools themselves).
Rủi ro:
Worth doing only if the order volume is large and stable enough, for long enough, to pay back the upfront tooling investment — short runs or low volume won't recoup it in time.
Bằng chứng tác giả đưa ra:
Measure the tool life of all 3 new drills, averaged over at least 5 tool-change cycles each. If the variation between measurements for the same drill is under 10%, the process is considered stable and safe to roll out.
Ý tưởng có thể tái sử dụng:
The "split a combined tool into separate single-purpose tools" principle also applies to: Form tools on lathes Form tools on milling machines The factory has already made this kind of change on a few other machines, but has never done a full plant-wide review to systematically roll this principle out. It was specifically the "Reusable Idea" field on Costdown that made it clear how much of this is still undone.
Dụng cụ / vật liệu dùng trong case này
- AGSTD16.0-60 — NACHI (TOOL_DRILL_CARBIDE)
- d5-20_d10-30_d20-15 — OTHER (TOOL_DRILL_CARBIDE)
- NF-GDN-06 — OSG (TOOL_DRILL_CARBIDE)
- NF-GDN-10 — OSG (TOOL_DRILL_CARBIDE)