How to Cut Machine Downtime, Inspection Cost and Scrap by Switching from a Power Chuck to a Collet Chuck - saving $1,228/year
Vấn đề thực trạng:
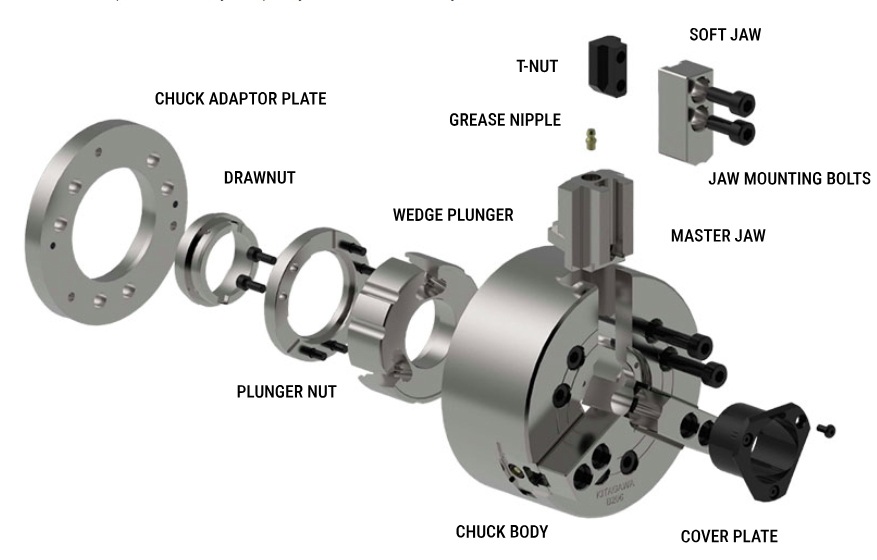
A lathe running a power chuck, on a product that's been in production year after year. The machine runs 3 shifts. About every 1–2 months, the chuck loses enough clamping force to hold the part — we call this chuck slip. When it happens, it shows up at different severity levels: - Mildest: the operator hears the abnormal sound and hits the emergency stop in time, so it's only the chuck that gets damaged. - Medium: it also damages about half a set of tool holders — around 2 holders. - Worst case: it damages 4 tool holders. After a chuck slip, maintenance has to re-true the chuck jaw face. If it's mild and the maintenance tech has experience with this machine, that alone can be done in about an hour. But the full clock — from the incident, to contacting maintenance, to maintenance fixing it, to sending the first article to QC, to QC measuring it, to getting the OK to restart the machine — takes at least 8 hours (one shift), and can run up to 2 working days. Sometimes maintenance is tied up elsewhere, or QC has a backlog of parts to measure. And that's not counting the times a chuck slips again shortly after QC has already cleared it and the machine is back running. Or times when, after the fix, the height dimension data comes back and fails Ppk — meaning it's back to re-truing the chuck, or replacing it outright. Maintenance can keep re-truing the same chuck multiple times, but to save cost they have to weigh whether to replace it instead. Put off replacement too long, though, and it ends up causing even more downtime. So the real cost here is large, but genuinely hard to put a number on and takes a lot of time to track, because there are too many variables involved.
Nguyên nhân gốc:
Right after the chuck jaw face is re-turned, it makes full, flush contact with the surface of the part being clamped. But after repeated clamping — about every 30 seconds per part — the wear adds up. Over a month, on 3 shifts, 8 hours a shift, 25 working days a month, at an operator efficiency of 0.87, this chuck clamps a part: ((8 × 60 × 60 × 3 × 25) / 30) × 0,87 = 62.640 times a month The power chuck has a lever-type internal component, and once that component wears down, the chuck face — as described above — stops making full-face contact with the part. Only a thin ring of contact is left. That drop in contact area is what reduces the clamping force, and that's what causes the chuck slip. Improvement mechanism You need to extend how long the chuck can hold full-face contact with the part. Keeping the same clamping mechanism only gets you so far — the real lever is cutting down the wear on the internal component that's causing the loss of full-face contact in the first place.
Cơ chế cải tiến:
You need to extend how long the chuck can hold full-face contact with the part. Keeping the same clamping mechanism only gets you so far — the real lever is cutting down the wear on the internal component that's causing the loss of full-face contact in the first place.
Giải pháp:
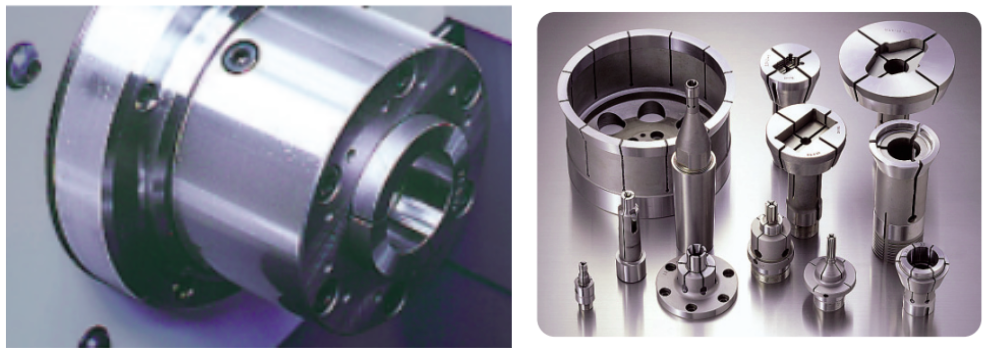
Switch entirely from a power chuck to a collet chuck.
Kết quả:
Trước cải tiến, các hạng mục chi phí đã khai trong đề án này tốn $764 mỗi tháng.
Sau cải tiến, cùng những hạng mục đó còn $662 mỗi tháng.
Mức tiết kiệm là $102 mỗi tháng, tương đương $1,228 mỗi năm — giảm 13.4% so với chi phí của chính những hạng mục đã khai trong đề án này (Nhân công (LABOR), Máy móc (MACHINE), Phế phẩm (SCRAP), Dụng cụ (CONSUMABLE)), không phải so với toàn bộ giá thành sản phẩm.
Vốn đầu tư là $212, khai chi tiết thành 1 khoản trong bảng chi phí triển khai một lần.
Thời gian hoàn vốn là 2.08 tháng.
Bài học kinh nghiệm:
Cranking up the chuck's clamping pressure right after a failure isn't a real long-term fix — it actually wears the chuck out faster. You can standardize how the chuck gets re-turned, find a faster way to do it, and cut down on first-article inspection and Ppk measurement. But since all of that only treats the symptom and not the root cause, it won't get you very far.
Tri thức tái sử dụng
Điều kiện áp dụng:
The investment cost for a full set of these chucks is fairly high. This matters especially if your plant has no other real products still running on power chucks that can't be converted to collet chucks — the power chucks you pull out become dead stock, and about the only thing you can do is resell them externally for very little. Retraining your technicians to switch from one clamping type to the other also takes a fair amount of time. Weighing everything gained against everything lost here is genuinely hard to pin down with numbers, which makes it a hard case to build when asking for approval to roll this out. Your production volume also needs to be high enough that you're never in a position where you have to stop this machine to switch over and machine a different part number.
Rủi ro:
This is a fairly big change, so the first time you apply it you'll be uneasy about it — especially if you can't track down the reason the previous engineers originally chose this type of chuck. They may well have had a reason. That said, you can go into it with some confidence: we've been running this conversion for close to 7 years now, and the results have held up well.
Bằng chứng tác giả đưa ra:
This one is fairly complex and slow, because you need to pull a lot of before-and-after data to make the comparison. If you wait until one machine has a fully clean dataset before rolling this out anywhere else, that just delays the benefit further. Here's what I'd suggest collecting — some of it's easy, some of it isn't, so weigh it out. You don't need all of it; you just need enough to get sign-off from management: - Time spent re-truing the chuck - Machine downtime caused by the incident - Cost of the chuck itself - Cost of the tooling used to re-true the chuck - Number of flanges replaced over at least a year, then converted to a monthly rate, counted against the number of machines actually running this way — keep in mind older machines will burn through flanges faster - Time spent measuring the first article - Time spent collecting the Ppk data
Ý tưởng có thể tái sử dụng:
Almost all of this transfers directly to any product with a long clamping length. "Long clamping" means the clamped length is more than twice the diameter — for example, if your part is Ø15, the clamped section needs to be at least 30mm. If anything here isn't clear, leave a comment below — a write-up like this can't fully capture everything that's in my head about this project.
Dụng cụ / vật liệu dùng trong case này
- Colllect chuck (TOOL_JIG_FIXTURE)
- Power chuck (TOOL_JIG_FIXTURE)
- X100 — TAKAMAZ (LATHE_CNC)