How to Stop Grooving Tool Chipping and Surface Scoring by Choosing a Deeper-Rated Insert for Better Chip Clearance saving $1,204
Vấn đề thực trạng:
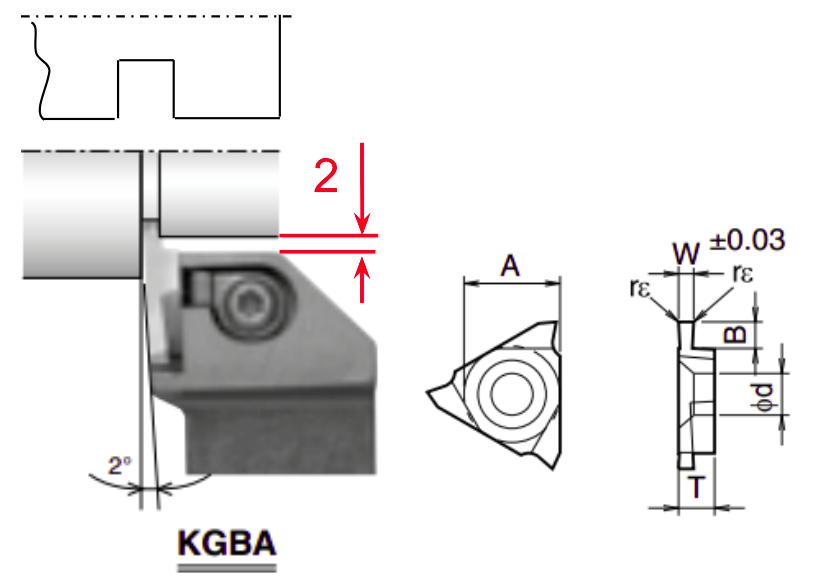
Grooving operation on a Ø15 blank. The tool manufacturer's recommended maximum cutting depth is 2 mm. Actual cutting depth in use was 1.3 mm, leaving 0.7 mm of unused depth. Tool life was not great. The part sometimes showed heavy scratching on the surface. Sometimes the insert chipped well before its expected life.
Nguyên nhân gốc:
The clearance between the workpiece and the tool shank was short (only 0.7 mm). This made it much more likely for fine chips to get wedged between the workpiece and the shank, causing the scratching. Sometimes a trapped chip would catch on the cutting edge and pull it, chipping the insert far earlier than its expected life.
Cơ chế cải tiến:
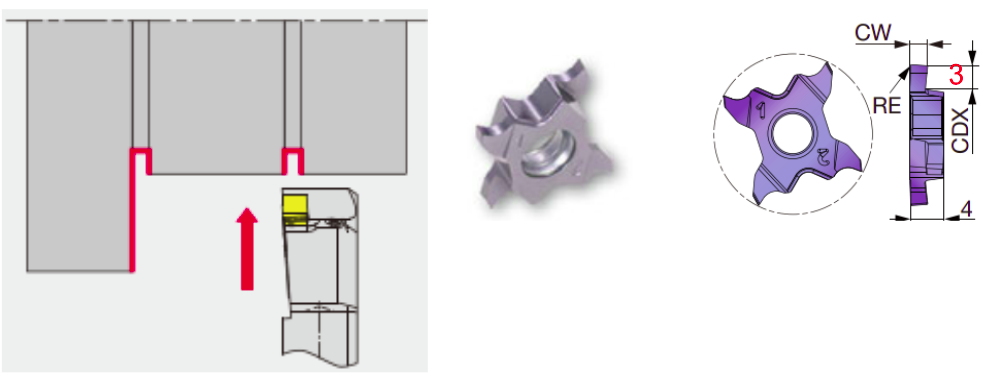
Increase the clearance between the tool shank and the workpiece so chips can evacuate more easily during machining.
Giải pháp:
Switch to an insert rated for a greater cutting depth.
Kết quả:
Trước cải tiến, các hạng mục chi phí đã khai trong đề án này tốn $548 mỗi tháng.
Sau cải tiến, cùng những hạng mục đó còn $448 mỗi tháng.
Mức tiết kiệm là $100 mỗi tháng, tương đương $1,204 mỗi năm — giảm 18.3% so với chi phí của chính những hạng mục đã khai trong đề án này (Dụng cụ (CONSUMABLE)), không phải so với toàn bộ giá thành sản phẩm.
Vốn đầu tư là $617, khai chi tiết thành 2 khoản trong bảng chi phí triển khai một lần.
Thời gian hoàn vốn là 6.15 tháng.
Bài học kinh nghiệm:
There were a lot of lessons here. I ran plenty of trials that mostly failed, or seemed to work for a moment without holding up — because they weren't aimed at the real root cause, which I hadn't found yet: - I used steel shims to seal off the gap between the tool shank and the tool post, because at the time I believed — and it did seem to be happening — that chips were running into that gap and packing in there. - I added more coolant nozzles, even though the coolant flow already looked sufficient. - I tried inserts with a better chipbreaker, hoping it would break the chips into smaller pieces and reduce chip wrapping. Then one story made the real root cause click. A tool vendor doing a trial run suggested an insert that I could tell, just by looking at it, wasn't going to work: First, it had no chipbreaker. The insert I was currently running did have one, and its tool life was already low. Second, its body was thinner than the insert I was currently machining with. I ran the trial anyway, for two reasons: I didn't want to turn down someone who'd given me a free insert to test, and because more than once in this job, reality had turned out very different from what I expected. The result floored me. The first edge alone lasted nearly double the tool life of the current insert, with no heavy surface scratching at all. And on both the part and the tool shank, there were no chips clinging to them afterward — the current insert, by contrast, always had chips packed on. It took me several days of thinking about it, because it was such an interesting result, before I landed on the real reason: this insert had a greater cutting depth. That's the opposite of what I originally assumed — that shorter and more rigid meant better. The truth is, an insert is already carbide, so it's already hard. There was one more interesting twist after that. Once I rolled this out across the whole product line, the new tool holder turned out to be expensive — around $35 a piece. I asked the supplier for a better price; they wouldn't budge, so I went looking for another manufacturer. The new supplier was Tungaloy. Switching over was straightforward, because I already had the real root cause in hand. If I'd had Costdown back then, I probably would have tracked this better and picked the first insert sooner — because I'd have been able to look at the tool-life curves of both suppliers side by side. I still feel for that first vendor. They were the ones who, without meaning to, helped me find the root cause I'm now sharing with everyone else.
Tri thức tái sử dụng
Điều kiện áp dụng:
None at all. Once you've found the real root cause, success follows as a matter of course.
Rủi ro:
I don't see any risk in this improvement.
Bằng chứng tác giả đưa ra:
This grooving tool has several cutting edges per insert, so a proper evaluation means tracking more than one edge: 5 edges per insert, so 5 inserts gives you 25 edges to track. Take the average tool life across all of them as the new baseline.
Ý tưởng có thể tái sử dụng:
This applies widely. Turning parts with a grooved profile are very common, so this generally transfers: increase the cutting depth of the tool. Whether you also want an insert with more cutting edges per piece is a separate call — that's up to you.
Dụng cụ / vật liệu dùng trong case này
- GB43R200 PR630 — KYOCERA (TOOL_INSERT_CNMG)
- TCP18R300-010 AH725 — TUNGALOY (TOOL_INSERT_CNMG)